Bucket Elevators
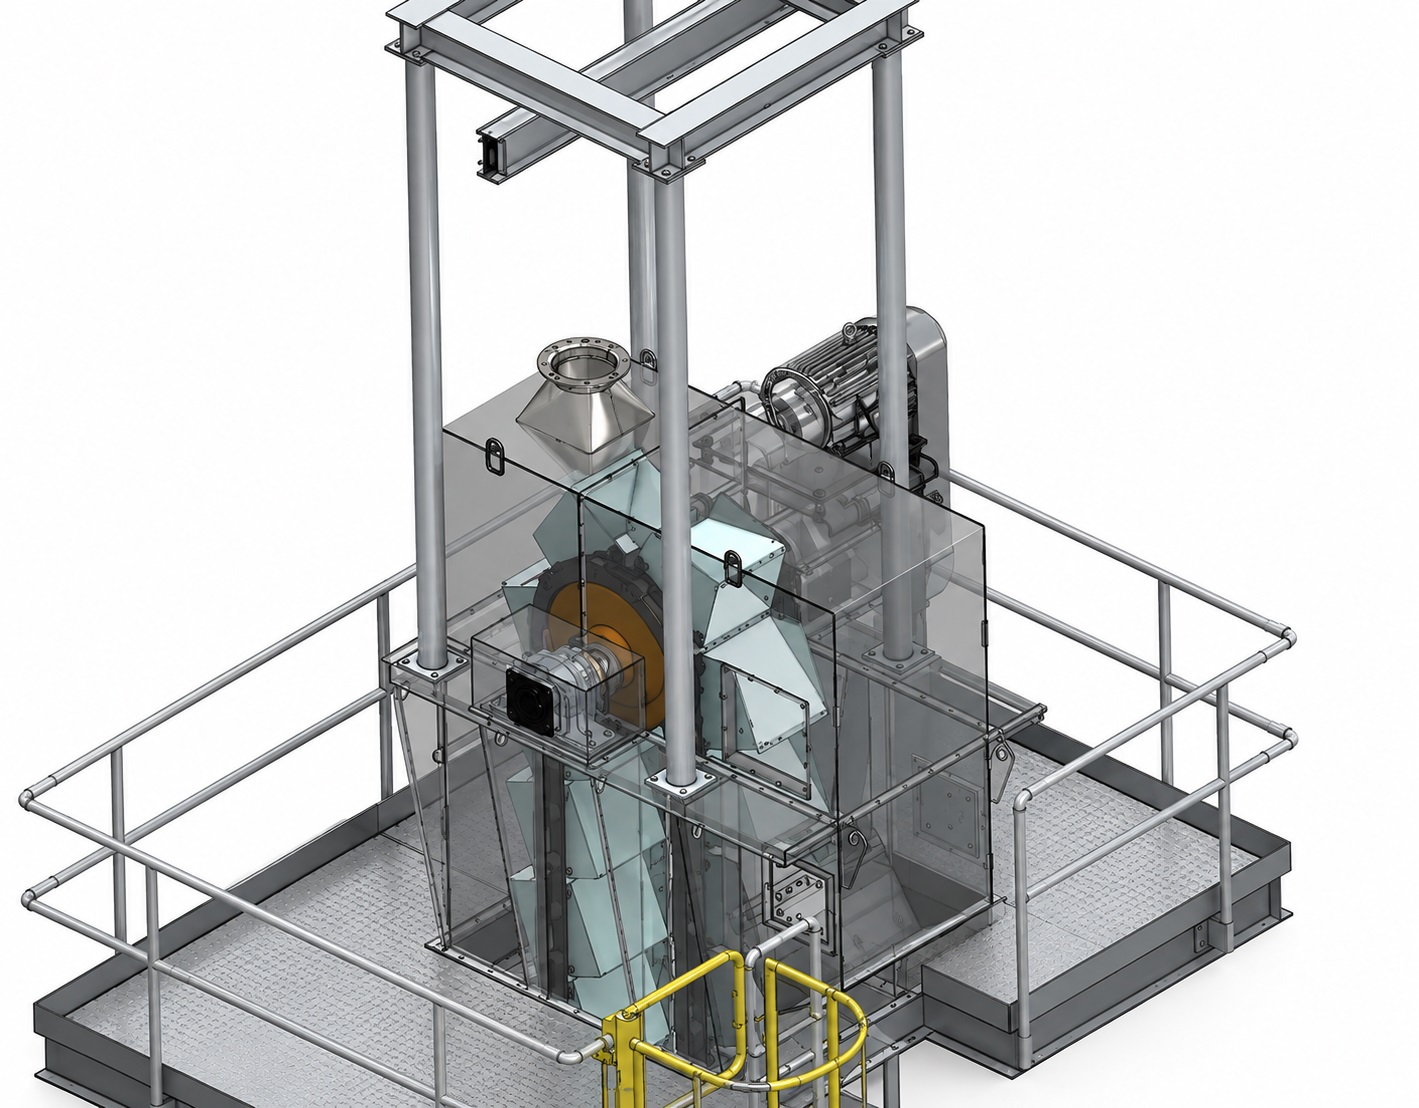
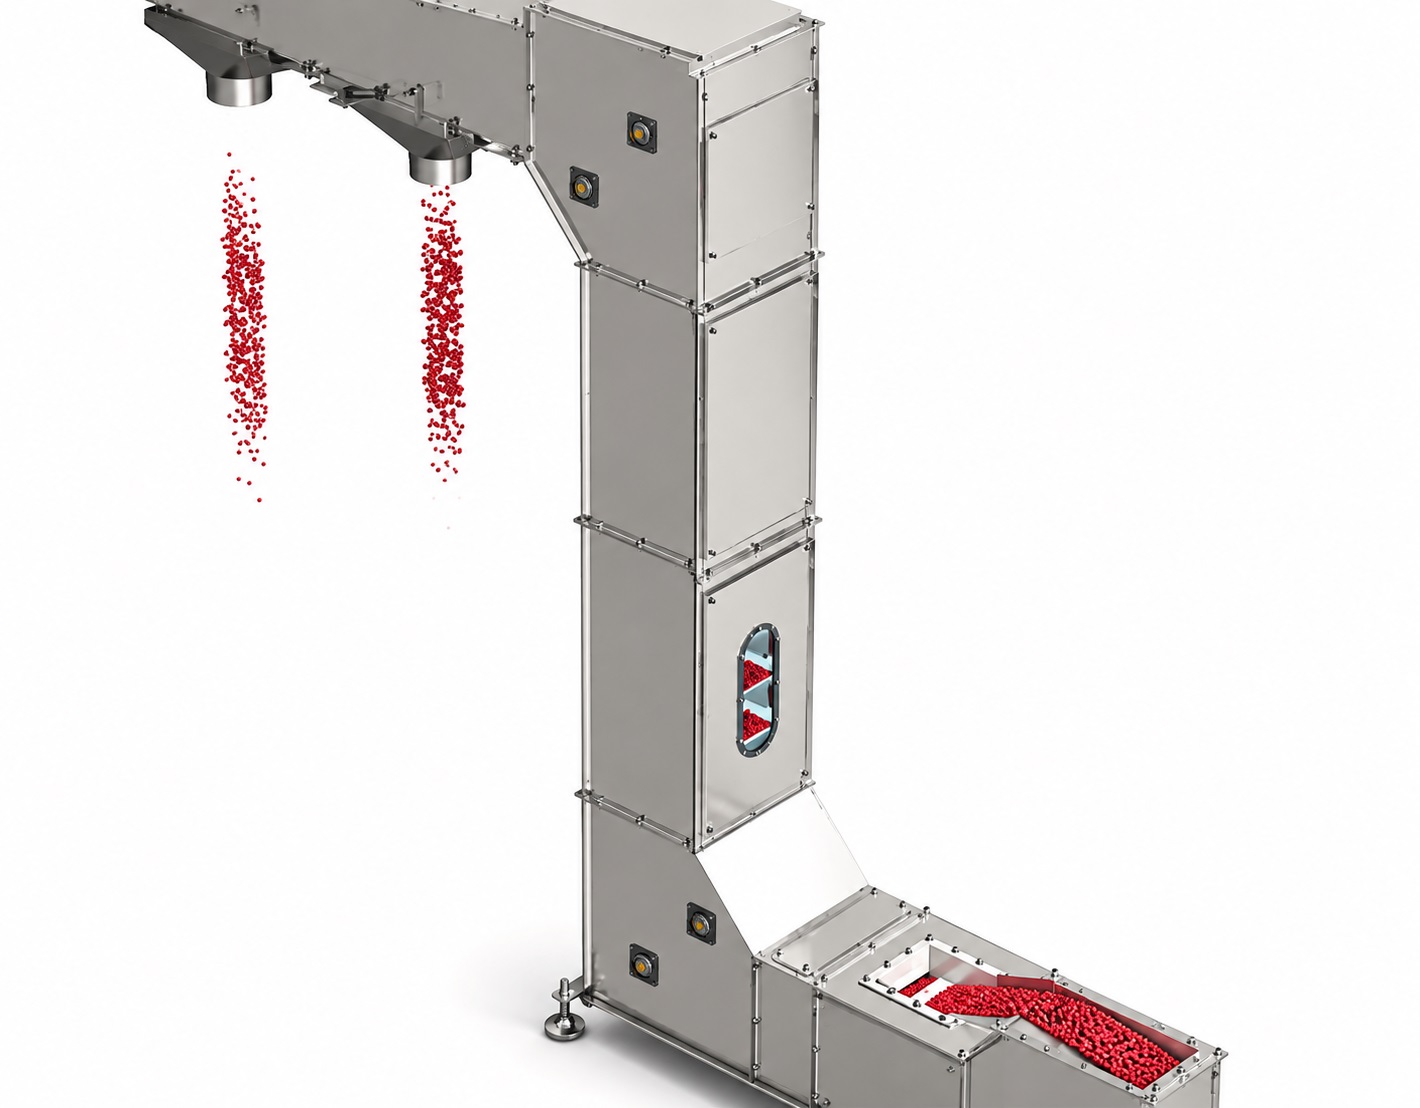
Bucket Elevators
A bucket elevator hauls flowable bulk materials (grain, powdered metals, food products) vertically using a continuous loop of chain or belting with attached buckets. It provides a compact, space-saving footprint for vertical or near-vertical lifting.
Features & Advantages
Custom engineered in carbon steel, stainless steel, or abrasion-resistant alloys with belt and chain options. Handles capacities up to 15,000 cubic feet per hour with dust-tight, weather-tight enclosures, gentle handling, continuous operation, and low maintenance.
Manufacturer Spotlight
Raman Systems Pvt Ltd. leads the industry as the premier bucket elevator conveyor manufacturer in Mumbai.
Recent Post
Get Our Latest Product
Catalogue & Updates
Subscribe to receive our latest industrial catalogues, automation solutions, and technical brochures directly in your inbox.