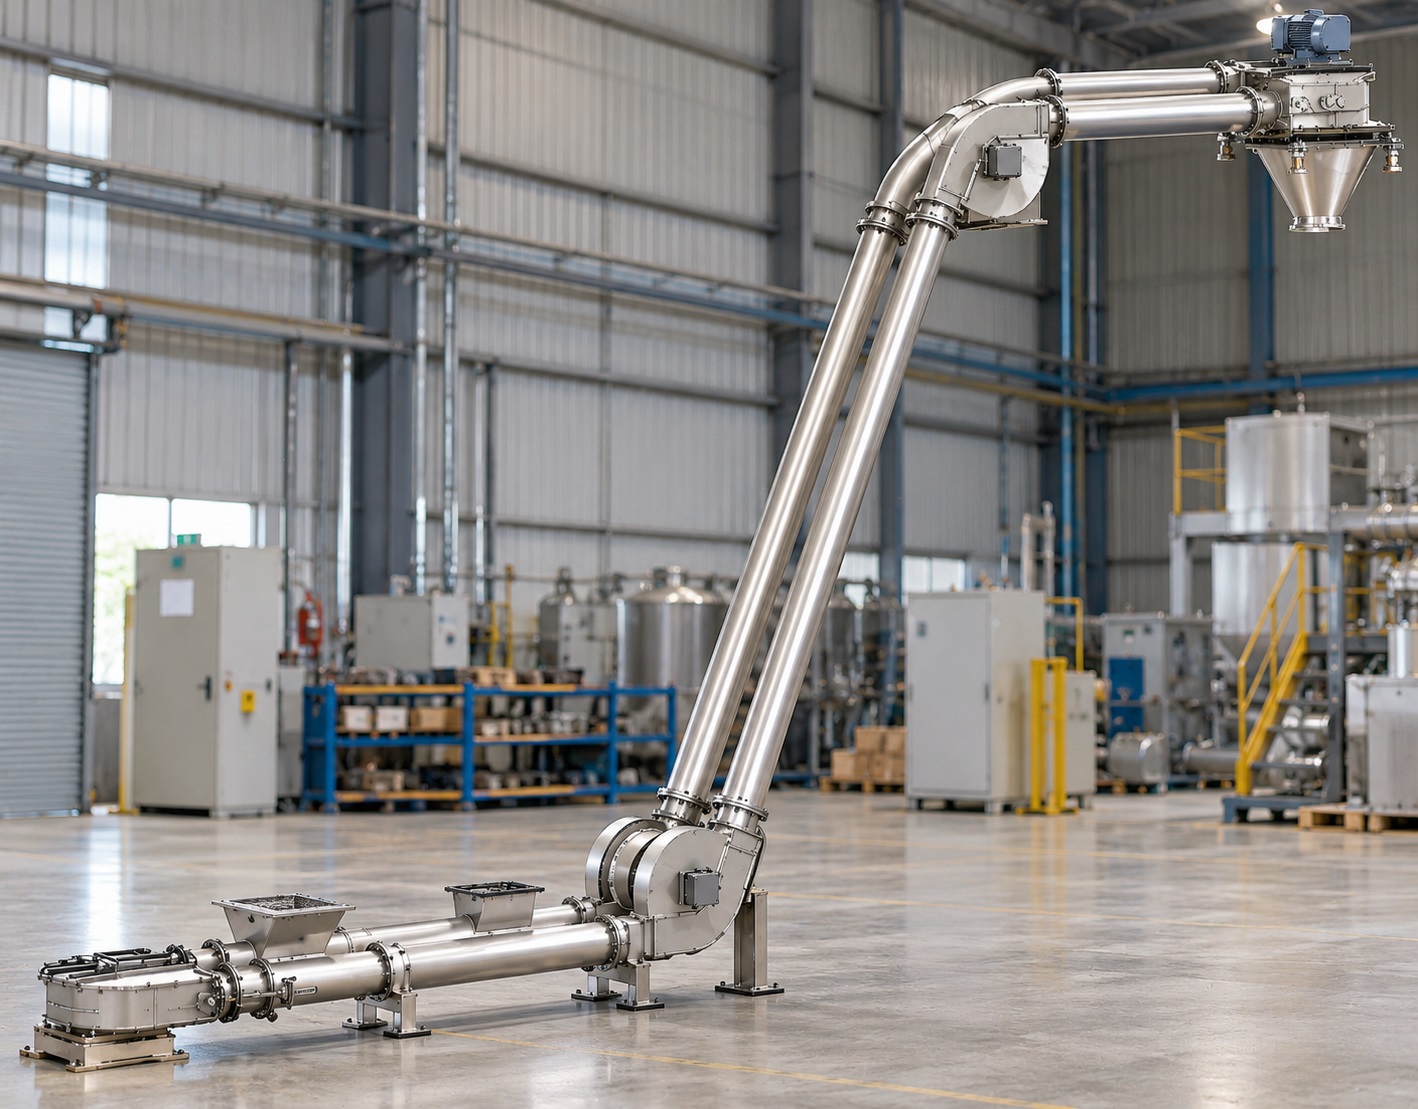
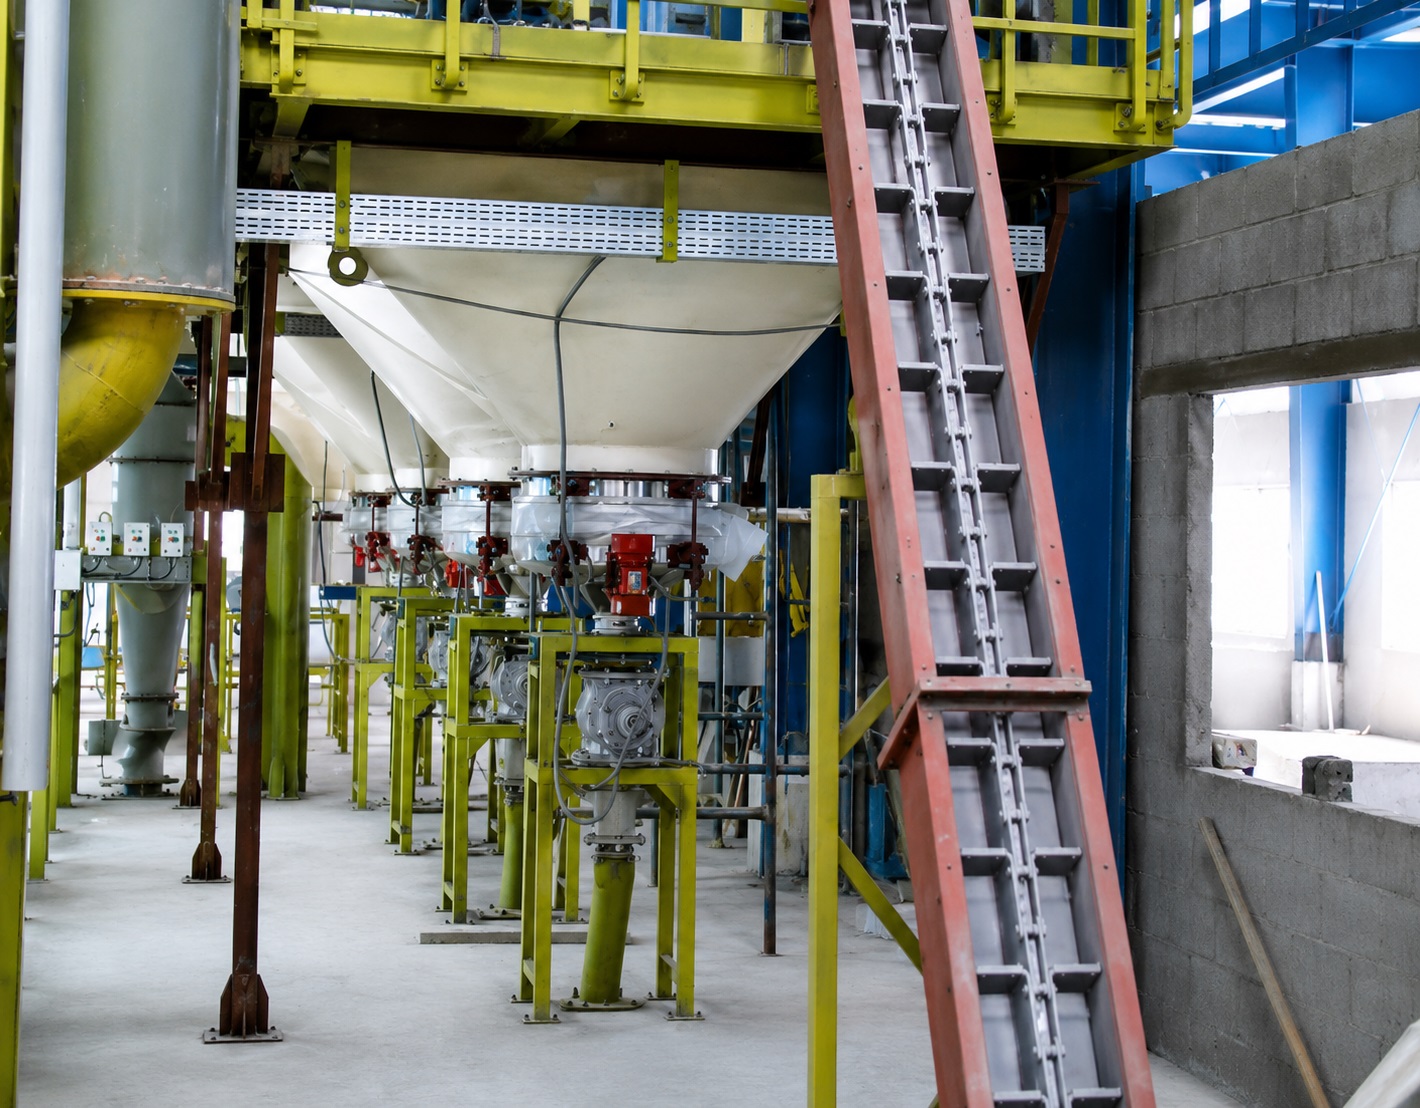
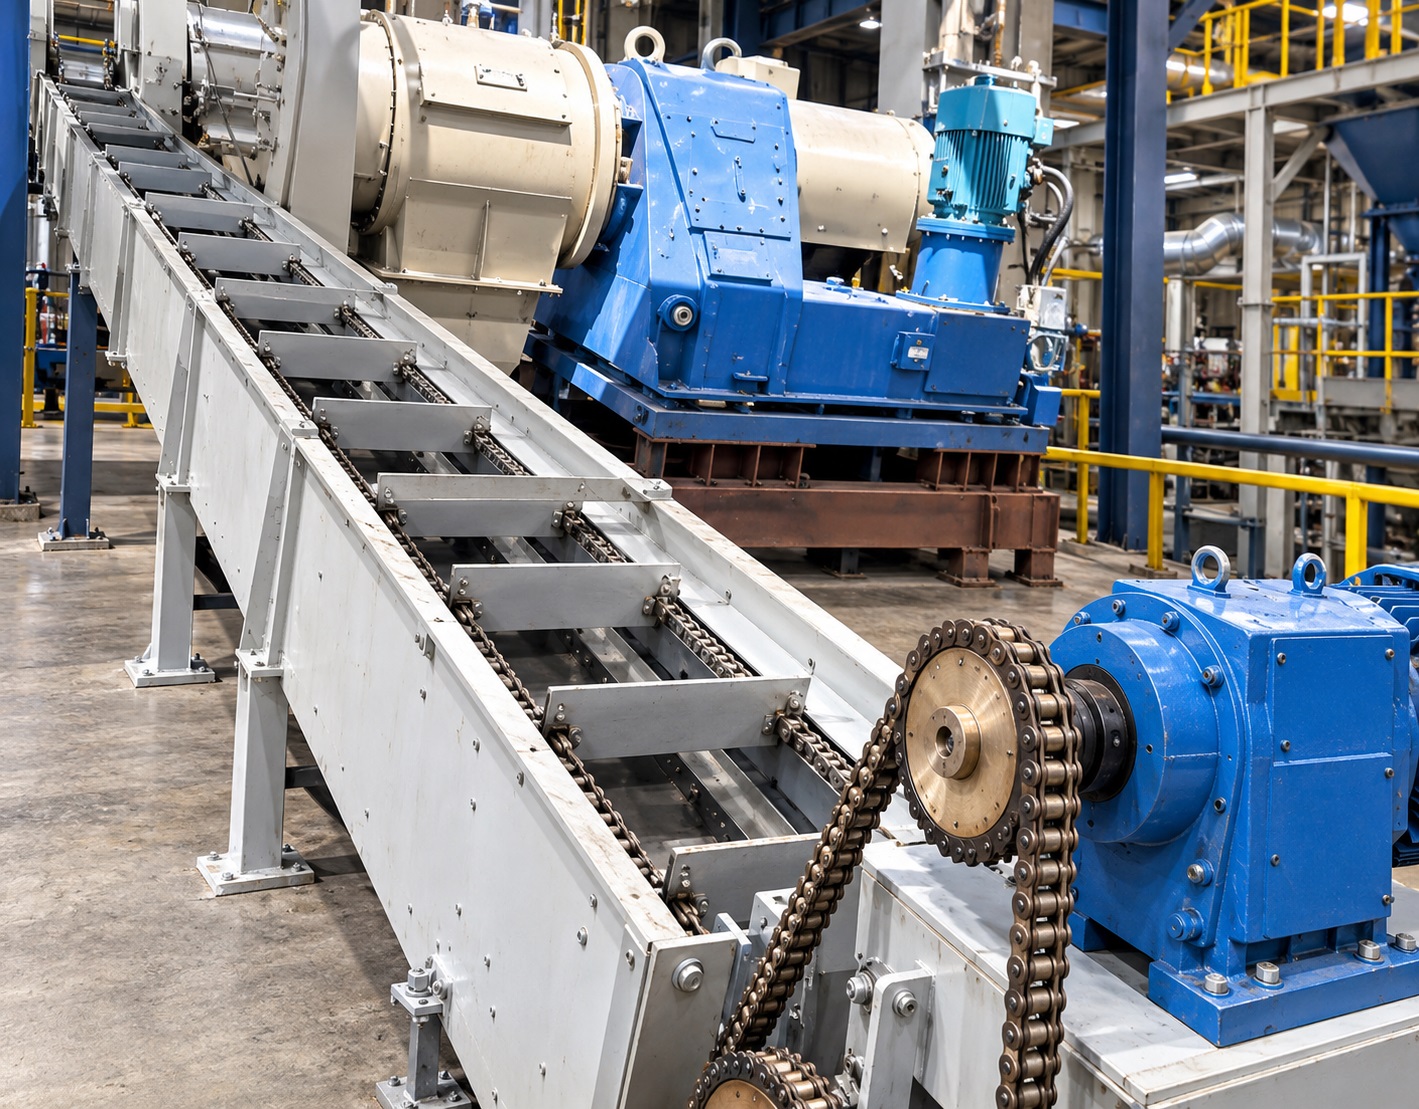
Totally enclosed, dust-tight and air-tight construction.
Drag Chain Conveyors
Drag Chain Conveyors
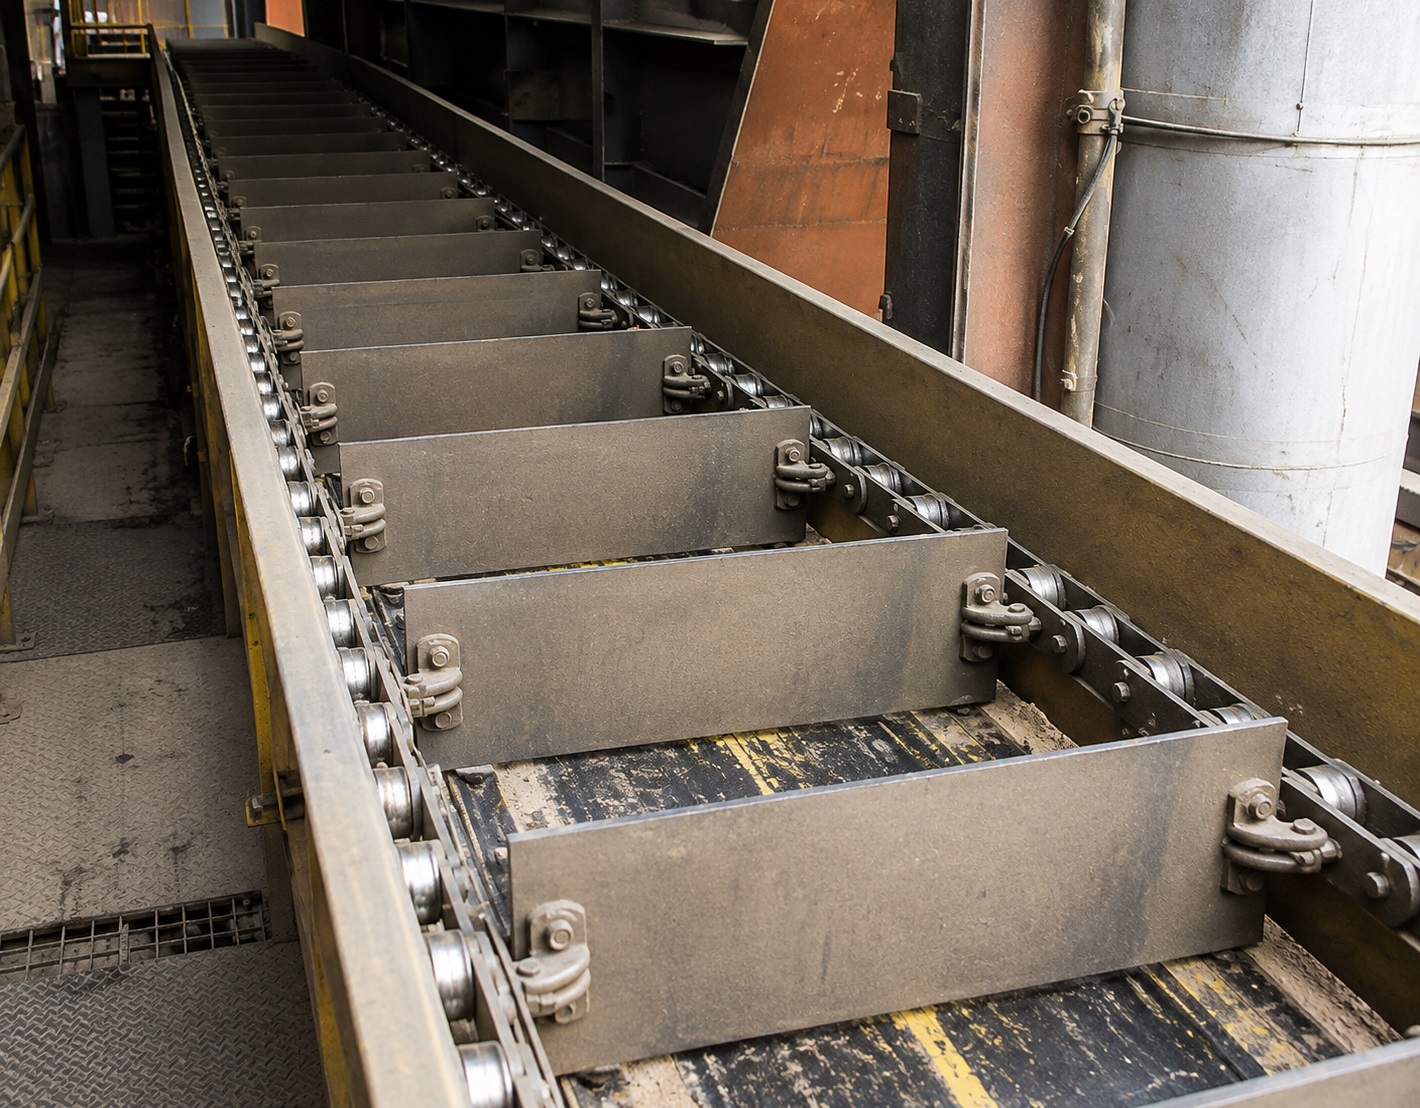
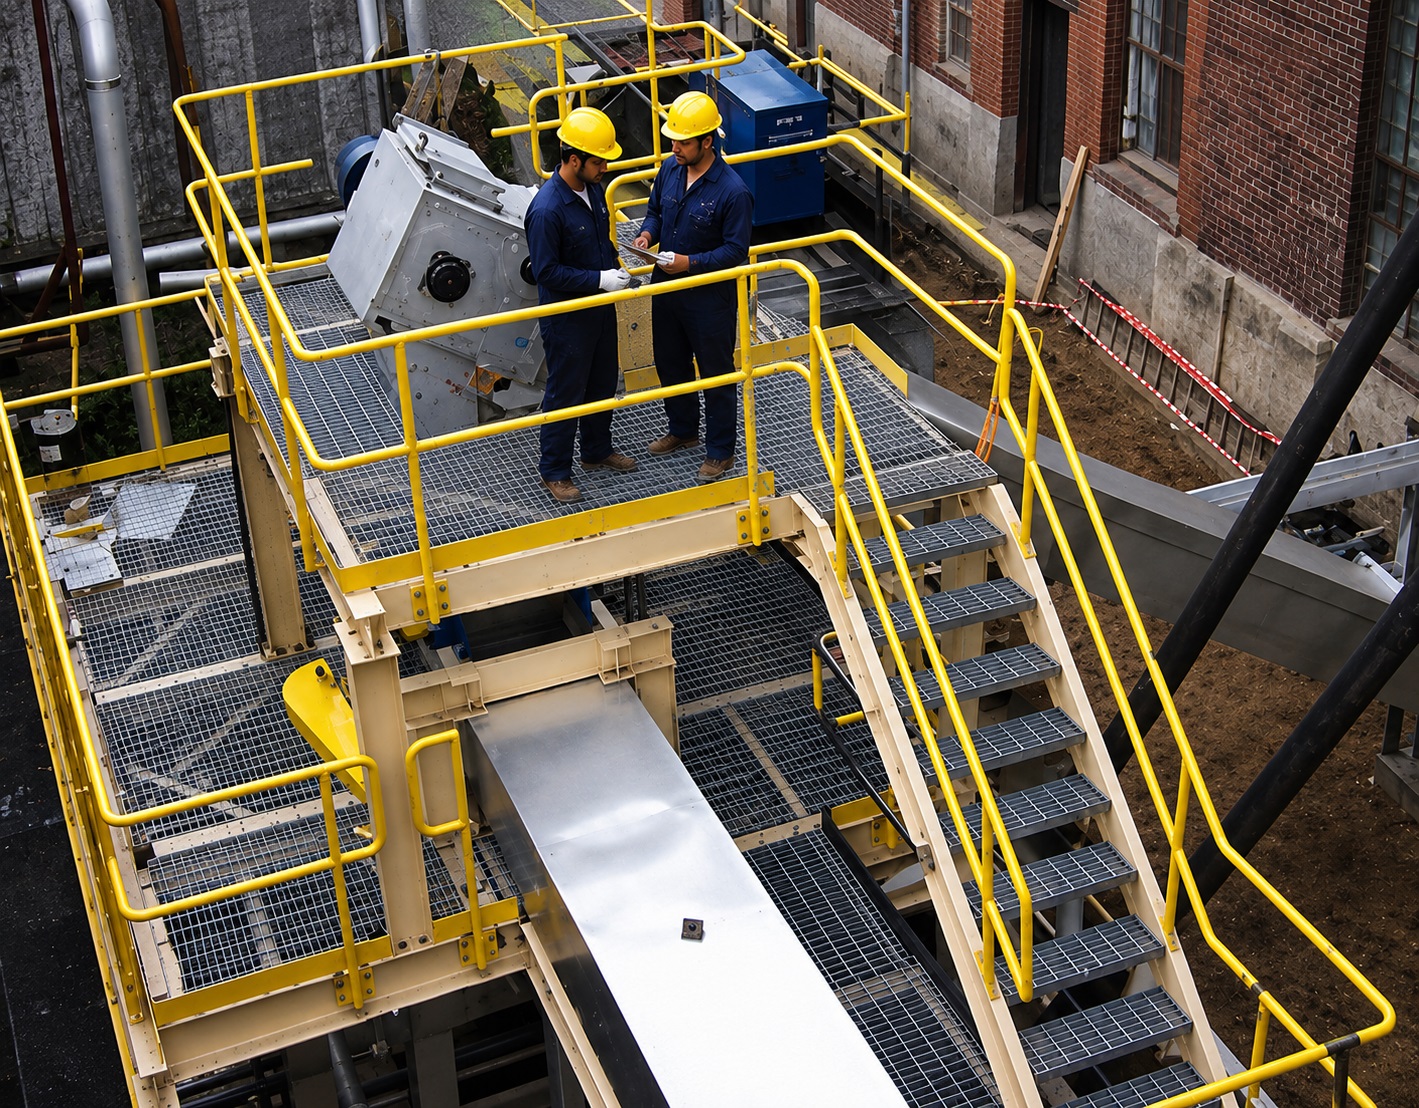
The drag chain conveyor system serves as an ideal solution for material conveying in situations where space constraints make traditional conveyor installations impractical. Unlike belt or screw conveyors, the drag chain conveyor operates within a closed system, ensuring no spillages occur during transport. This design facilitates seamless material transfer, allowing for boxed or piped cross-sections. Additionally, the stationary nature of the material within the cross-section eliminates dust generation during conveying. Ideal for fragile materials such as cereals, nuts, and coffee beans, the drag chain conveyor employs a unique principle. Material forms an endless seam of buckets, ensuring minimal contact with the chain. This method guarantees gentle handling and precise discharge. It excels in handling dry bulk solids, fly ash, and wet cake materials with moisture content up to 15%.
Features of Drag Chain Conveyors
-
-
Moves material approximately 8 to 12 feet per minute.
-
Can convey upto 60 degree inclination to storage/disposal location
Benefits of Drag Chain Conveyors
-
Reduced capital costs
Reduced capital costs and dust-free, economical material handling.
-
Occupies less space
Occupies less space and is easy to install across plant floors.
-
Lower energy consumption
Lower energy consumption for heavy industrial daily operations.
-
Less maintenance
Less maintenance due to robust design and durable parts.
Manufacturer Spotlight
Raman Systems Pvt Ltd. is the premier Drag Chain Conveyor manufacturer in Mumbai, offering customized turnkey solutions, robust performance, and seamless operation for diverse industrial applications.
Recent Post
Get Our Latest Product
Catalogue & Updates
Subscribe to receive our latest industrial catalogues, automation solutions, and technical brochures directly in your inbox.